High-Precision Electrical Discharge Machining (Wire EDM & Sinker EDM) Services
Graphler Manufacturing Solutions delivers high-precision Electrical Discharge Machining (EDM) solutions for complex shapes, sharp internal corners, deep cavities, and hard-to-machine materials that conventional machining methods cannot achieve.
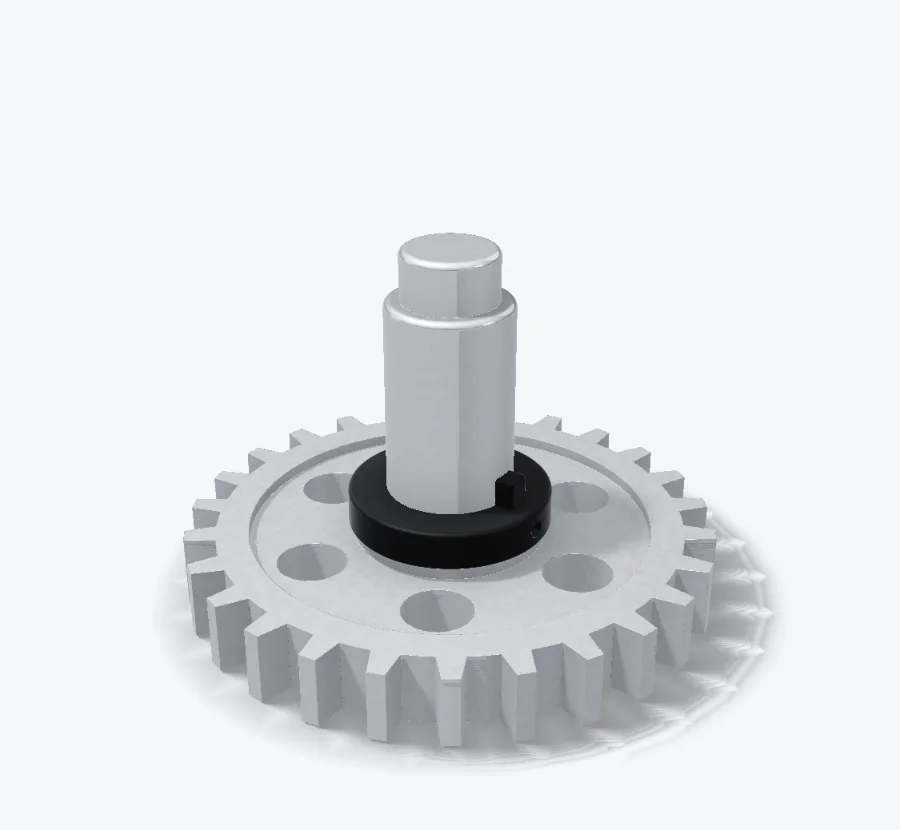
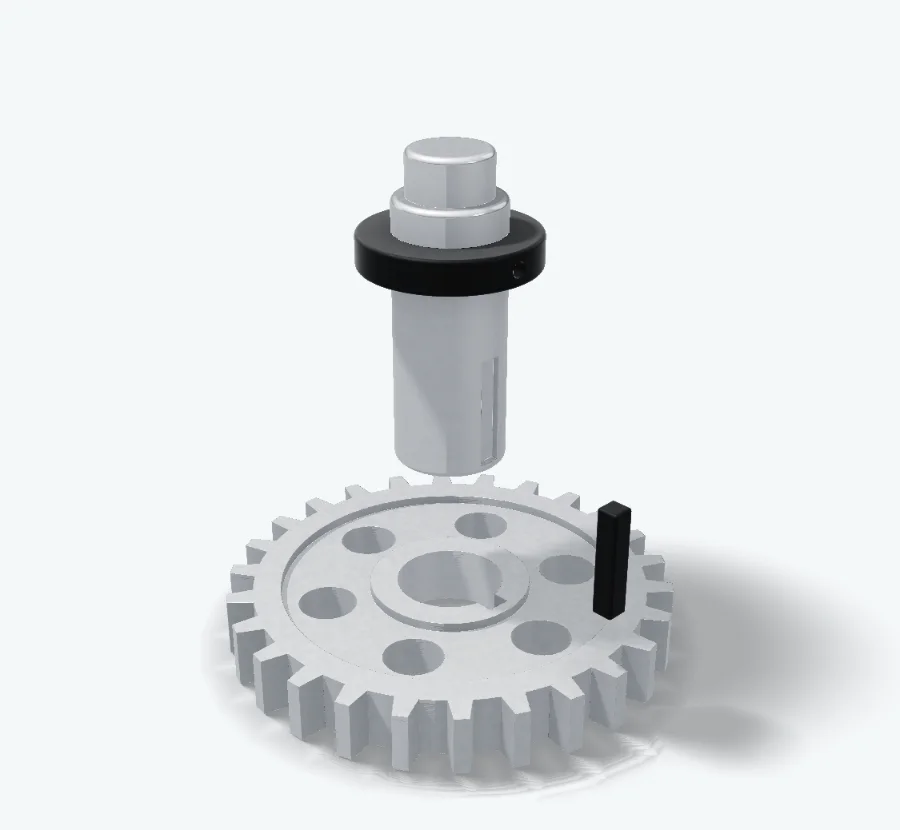
- Spur gear
- Shaft
- Key
- Collar
Advanced Spark Erosion Machining for Extreme Precision & Intricate Detail
When components require sharp internal radiuses, narrow slots, complex extrusion dies, or machining through fully hardened metal alloys, traditional rotary cutting tools encounter physical limits. At Graphler, our Electrical Discharge Machining (EDM) facility utilizes controlled electrical spark erosion to melt and vaporize material with micron-level precision, without exerting mechanical cutting forces on the workpiece.
Precision Wire EDM (Wire-Cut EDM)
High-accuracy CNC wire cutting utilizing a continuously moving metallic wire electrode to slice intricate 2D and tapered 3D contours through conductive materials.
Sharp Internal Corners & Fine Slots
Machining tight internal radiuses and narrow keyways impossible to produce with milling cutters.
Thick Stack & Tall Part Cutting
Maintaining straight vertical walls and exact geometry across thick workpiece plates.
Taper & Multi-Axis Contour Cutting
Independent 4-axis movement for complex top-to-bottom transitional profiles.
Burr-Free Edge Quality
Clean spark erosion that leaves zero mechanical burrs or edge distortion.
Sinker EDM (Ram / Plunge EDM)
Precision cavity sinking utilizing custom-machined graphite or copper electrodes to burn negative shapes, deep blind pockets, and complex mould details.
Deep Cavity & Blind Pocket Machining
Sinking complex shapes into hardened steel blocks without tool deflection.
Tool & Die and Injection Mould Inserts
Producing intricate core/cavity details, rib slots, and textured surface finishes for moulds and stamping dies.
Micro-Detailing & Intricate Geometries
Burning fine ribs, internal splines, and high-aspect-ratio features.
Machining Hard-to-Machine Alloys & Hardened Metals
Because EDM is a non-contact thermal erosion process, material hardness does not limit machining capability. We process pre-hardened alloys without causing structural distortion or thermal stresses associated with traditional cutting.
Hardened Steels & Tool Steels
Supported Materials & Alloys
Typical Precision Components
Carbides & Superalloys
Supported Materials & Alloys
Typical Precision Components
Conductive Metals & Alloys
Supported Materials & Alloys
Typical Precision Components
Manufacturability Optimization & In-House Tooling Expertise
Our engineering team works directly with technical leads to optimize part designs and electrode paths, reducing burn time and lowering overall component costs.
Design for Manufacturability (DFM)
Early-stage CAD evaluation to optimize spark gaps, flush hole placement, and wire entry points.
Electrode Design & Fabrication
In-house CNC milling of high-density graphite and copper electrodes for Sinker EDM applications.
Prototype to Production Scalability
Supporting single-unit tool development and rapid prototyping through to production-scale component runs.
Micron-Level Precision and Rigorous Quality Control
Precision components manufactured via Wire and Sinker EDM undergo strict dimensional verification to guarantee compliance with specified drawing tolerances.
ISO 9001 Compliant Quality Workflow
Structured process documentation and quality control at every stage of production.
Dimensional Inspection
Measurement verification of critical profiles, slot widths, and hole locations using modern inspection systems.
Full Material Traceability
Complete batch material test reports (MTRs) and material certifications provided with orders.
Export-Compliant Packaging
Protective rust-inhibitive packaging and global logistics management ensure damage-free delivery.
Our Systematic Manufacturing Workflow
- Step 01
Express Quoting
Upload CAD files for fast pricing supported by a two-stage technical feasibility review.
- Step 02
Order Confirmation & DFM
Engineering review to finalize drawing specifications, tolerances, and electrode tooling plans.
- Step 03
Controlled EDM Machining
Execution on modern Wire and Sinker EDM equipment in a controlled shop environment.
- Step 04
Quality Inspection
Dimensional verification against strict drawing callouts using modern measuring systems.
- Step 05
Global Shipping
Export-compliant packaging, rust prevention, and worldwide logistics support.
- Step 06
Real-Time Order Tracking
Complete visibility with real-time status updates and direct access to inspection reports via our online portal.
Technical questions about Wire & Sinker EDM
When should I choose Wire or Sinker EDM over conventional CNC milling?
Electrical Discharge Machining (EDM) is recommended for parts made from hardened metals (like tool steels or carbides), components requiring sharp internal corners or deep narrow slots, and intricate tool/die cavities that milling cutters cannot physically reach or cut without breaking.
What level of tolerance and accuracy can Graphler achieve with EDM?
Depending on part geometry and material specifications, our EDM processes achieve ultra-tight tolerances as low as ±0.0001 inches (±0.002 mm).
Which CAD file formats are accepted for an express quote?
You can upload your 3D CAD models and 2D engineering drawings directly through our quote portal in STEP (.stp), IGES (.igs), STL (.stl), or .ZIP file formats.
Submit Your 3D CAD File for an Express Quote
Ready to manufacture complex, hard-to-machine precision components? Partner with Graphler Manufacturing Solutions for high-accuracy Wire & Sinker EDM services.